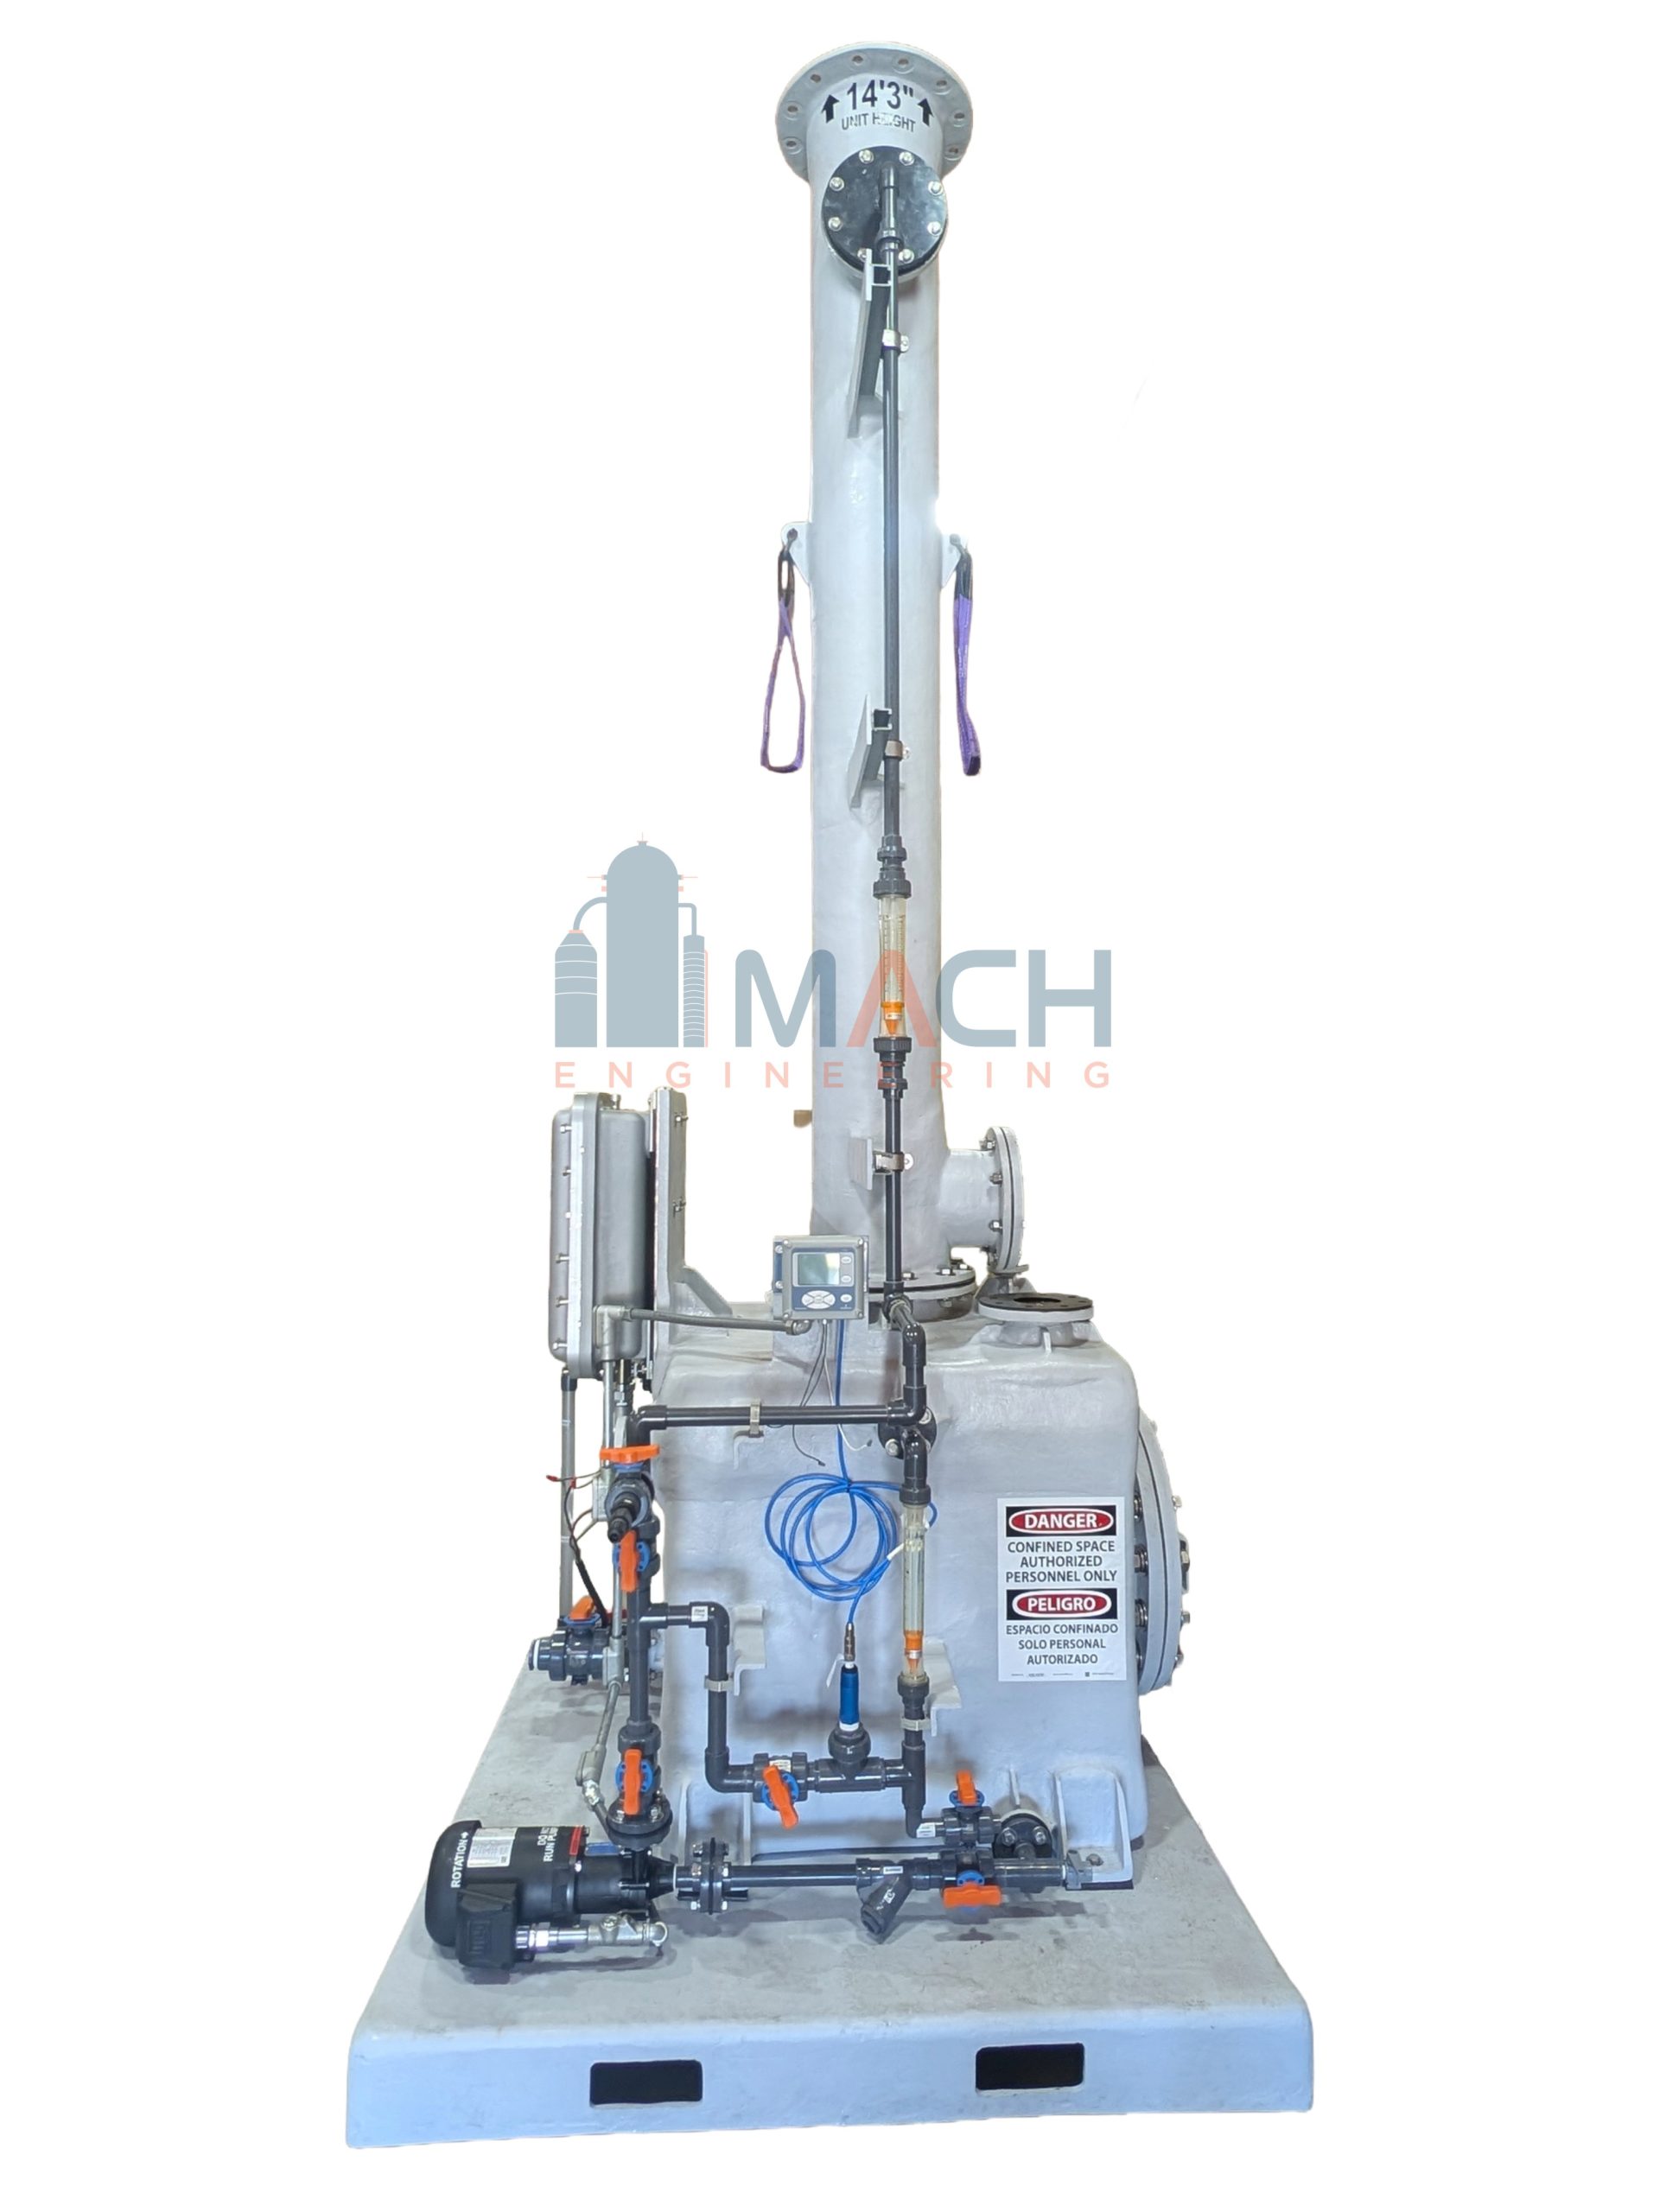
Initial Challenge / Problem
Treat reactor vent gas containing NOx and trace mercury vapor from batch operations.
| Industry of Client | Waste disposal / chemical processing |
| Type of Pollutants | NOx (primary), Hg vapor (trace), HNO₃, HCl, NOCl, Cl₂ |
| Material | 316L stainless steel |
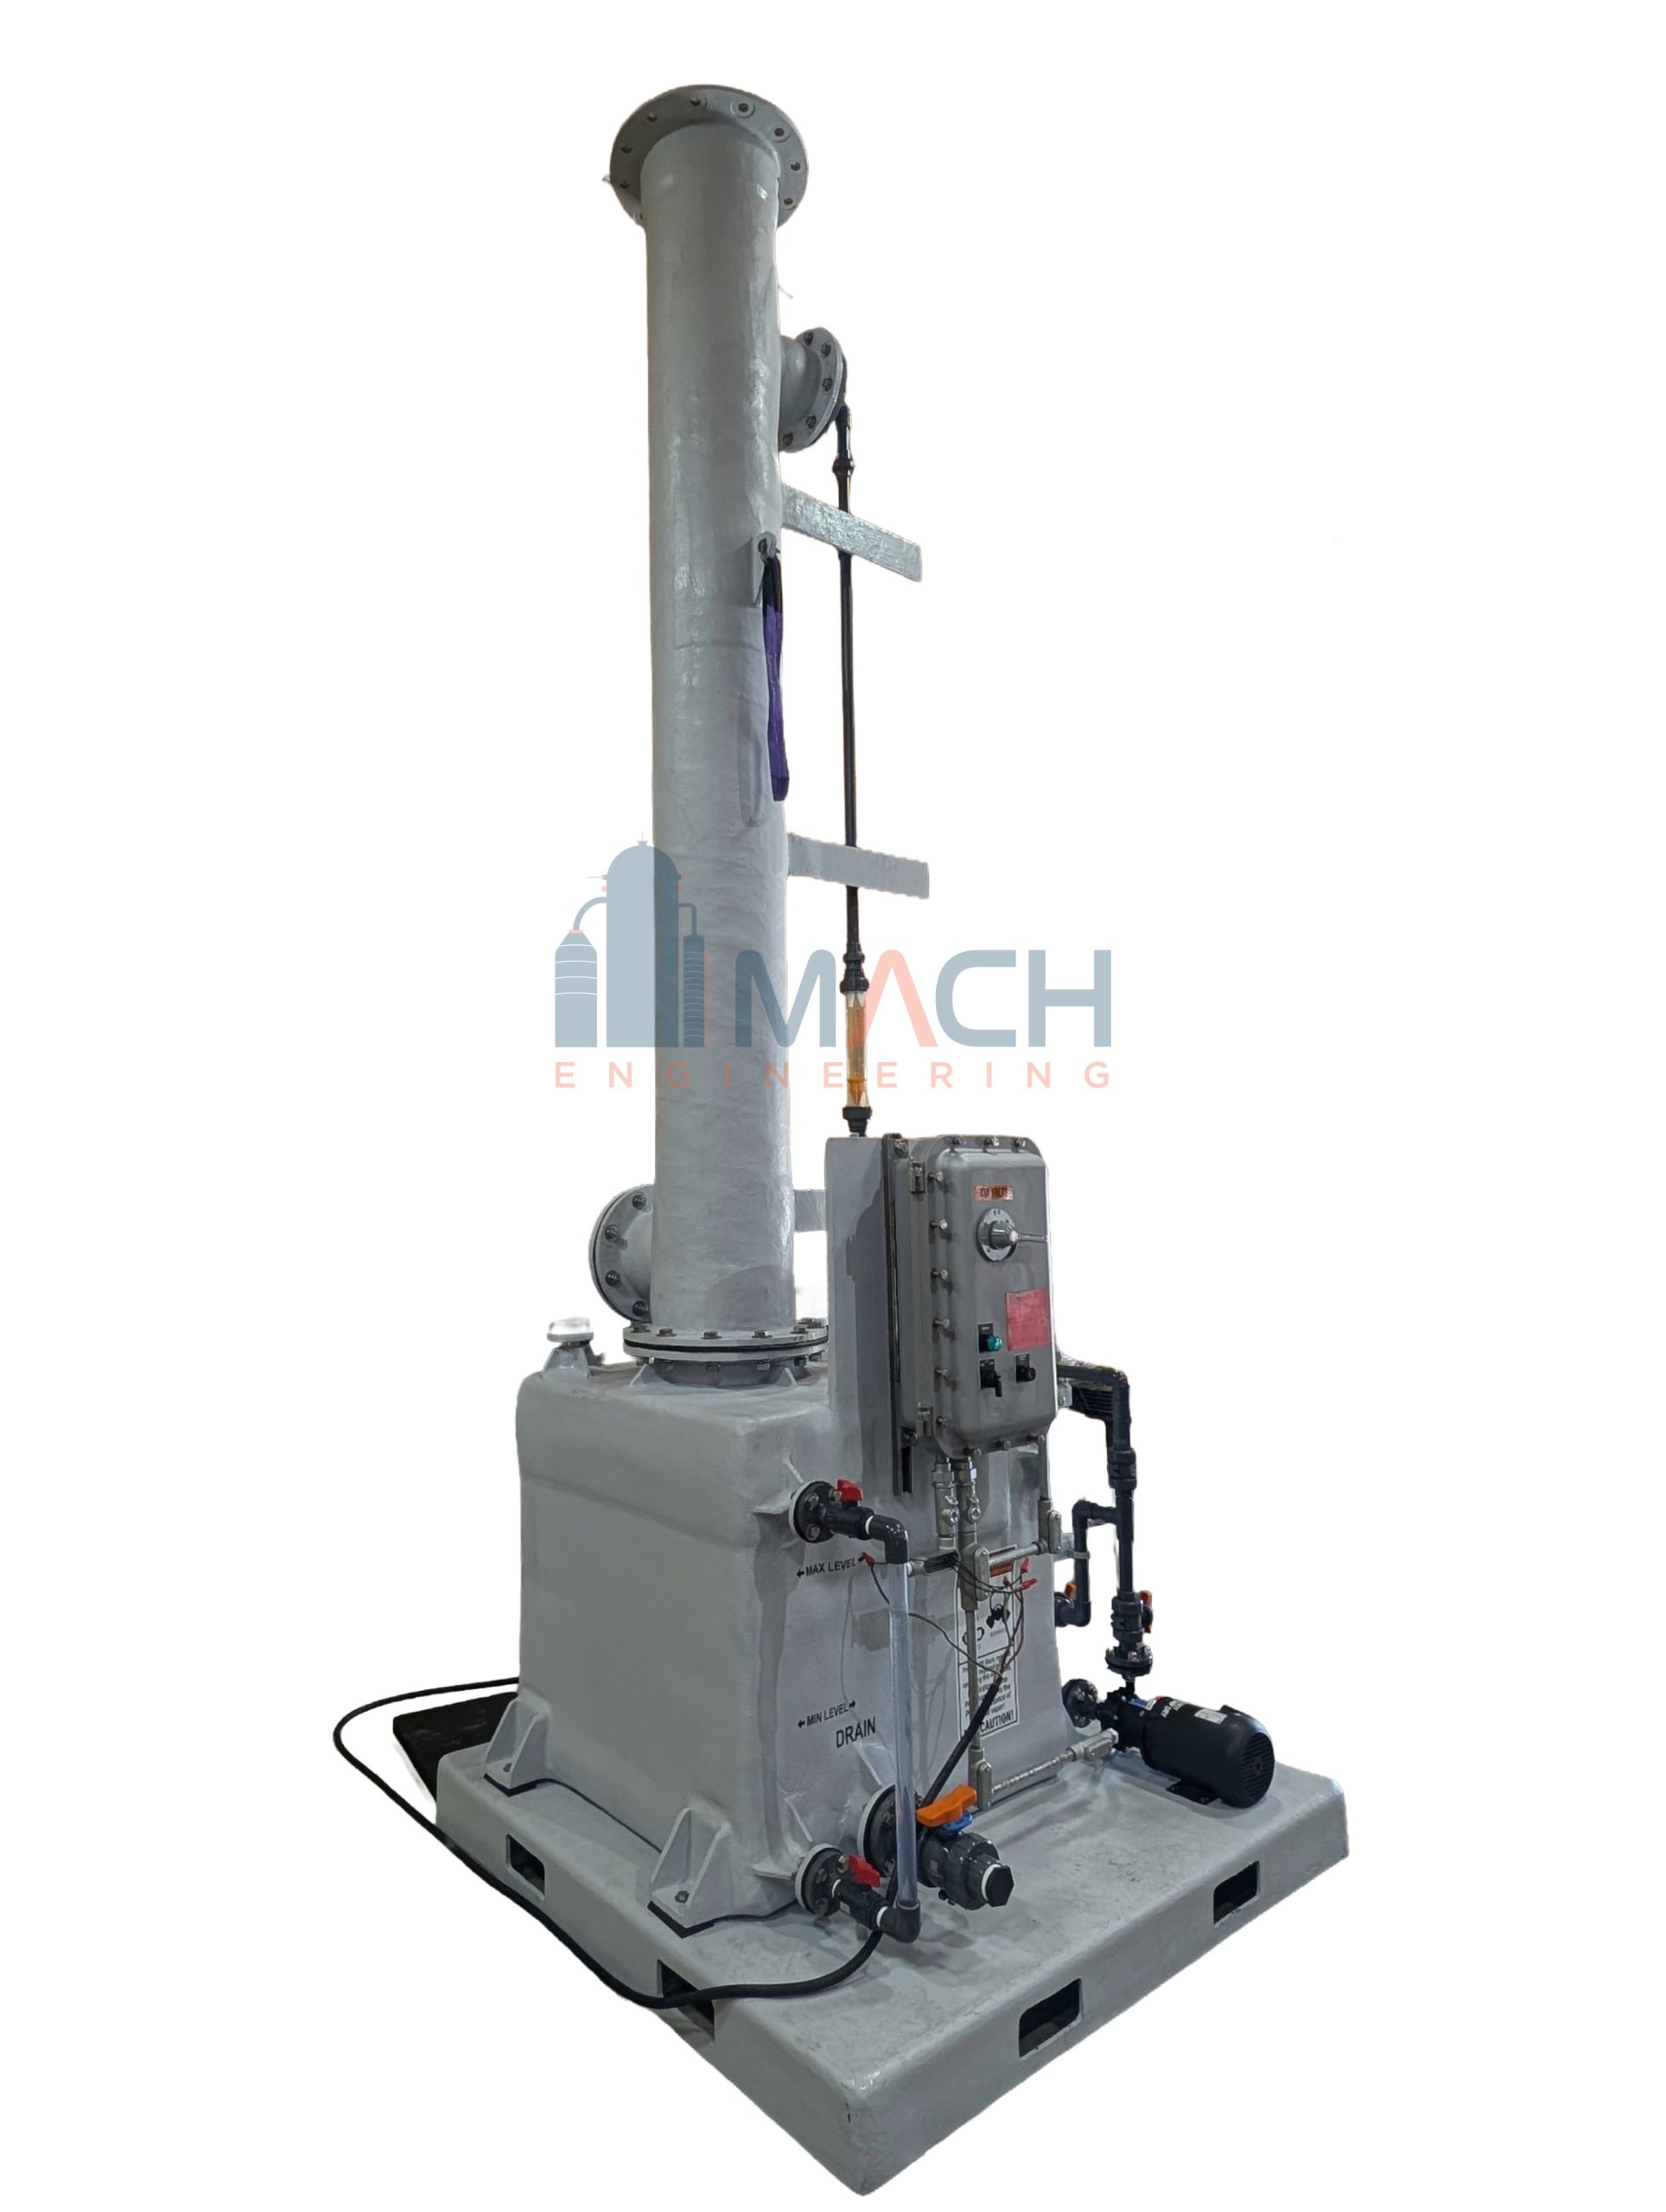
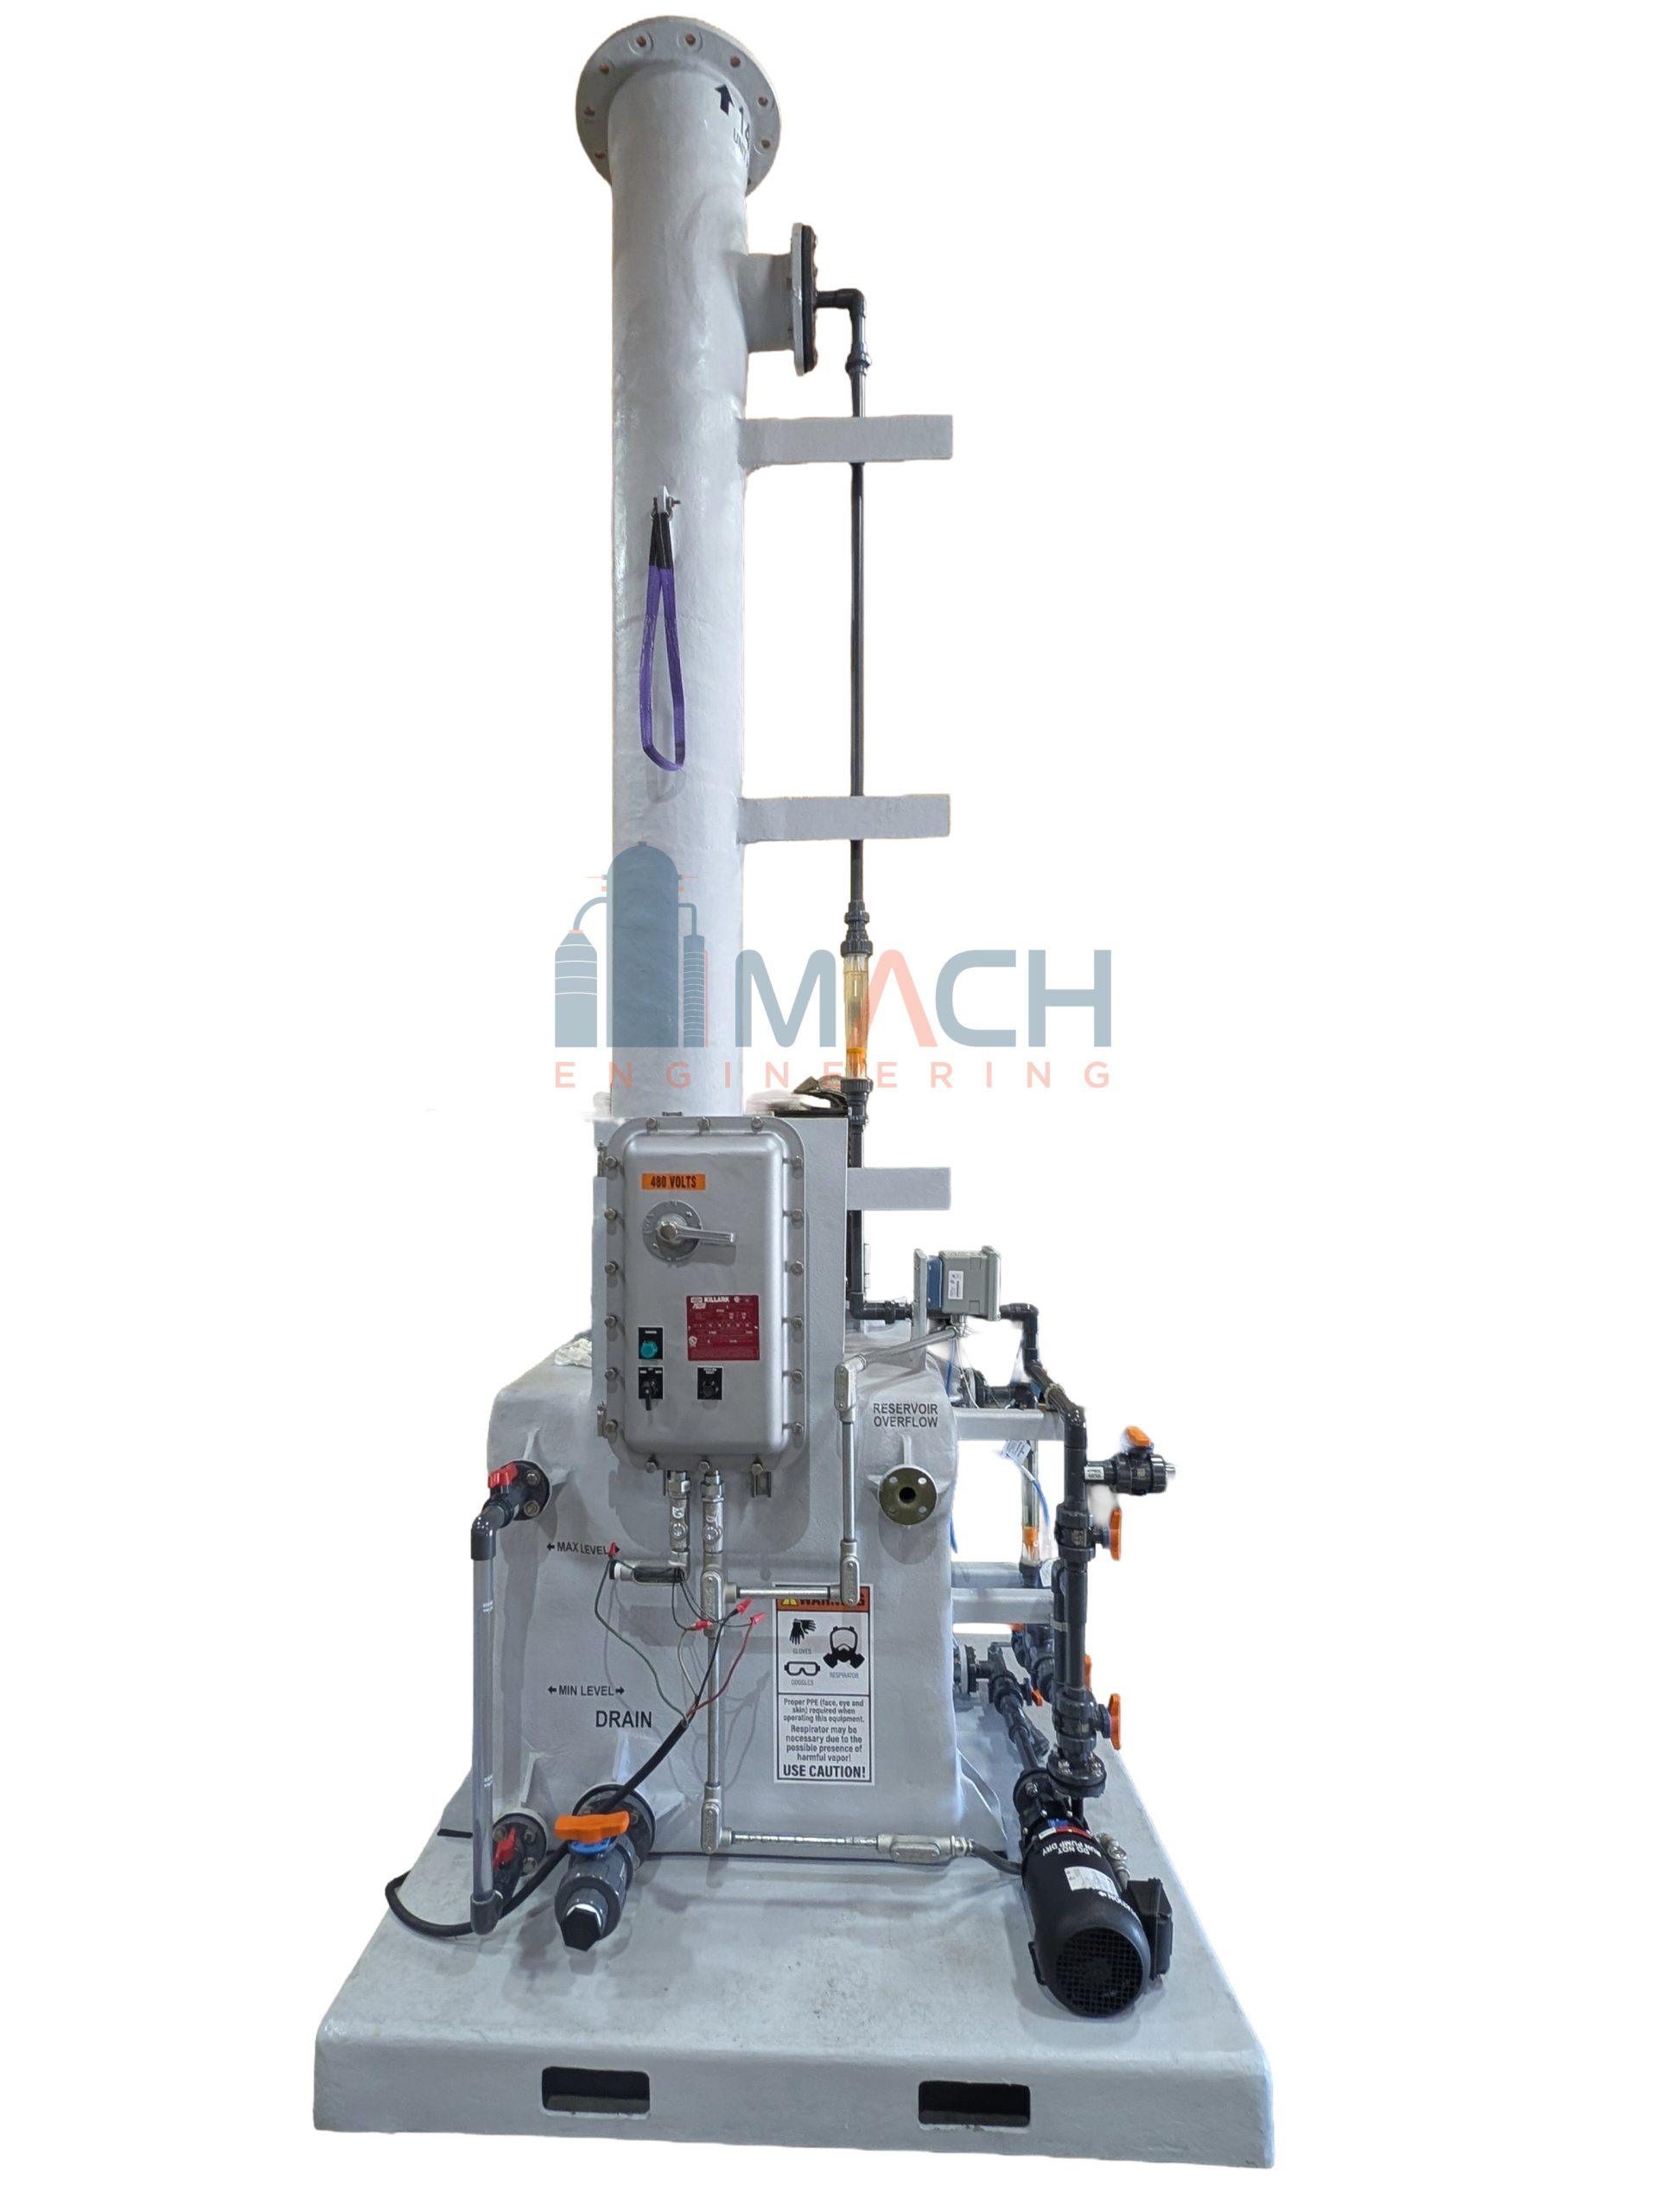
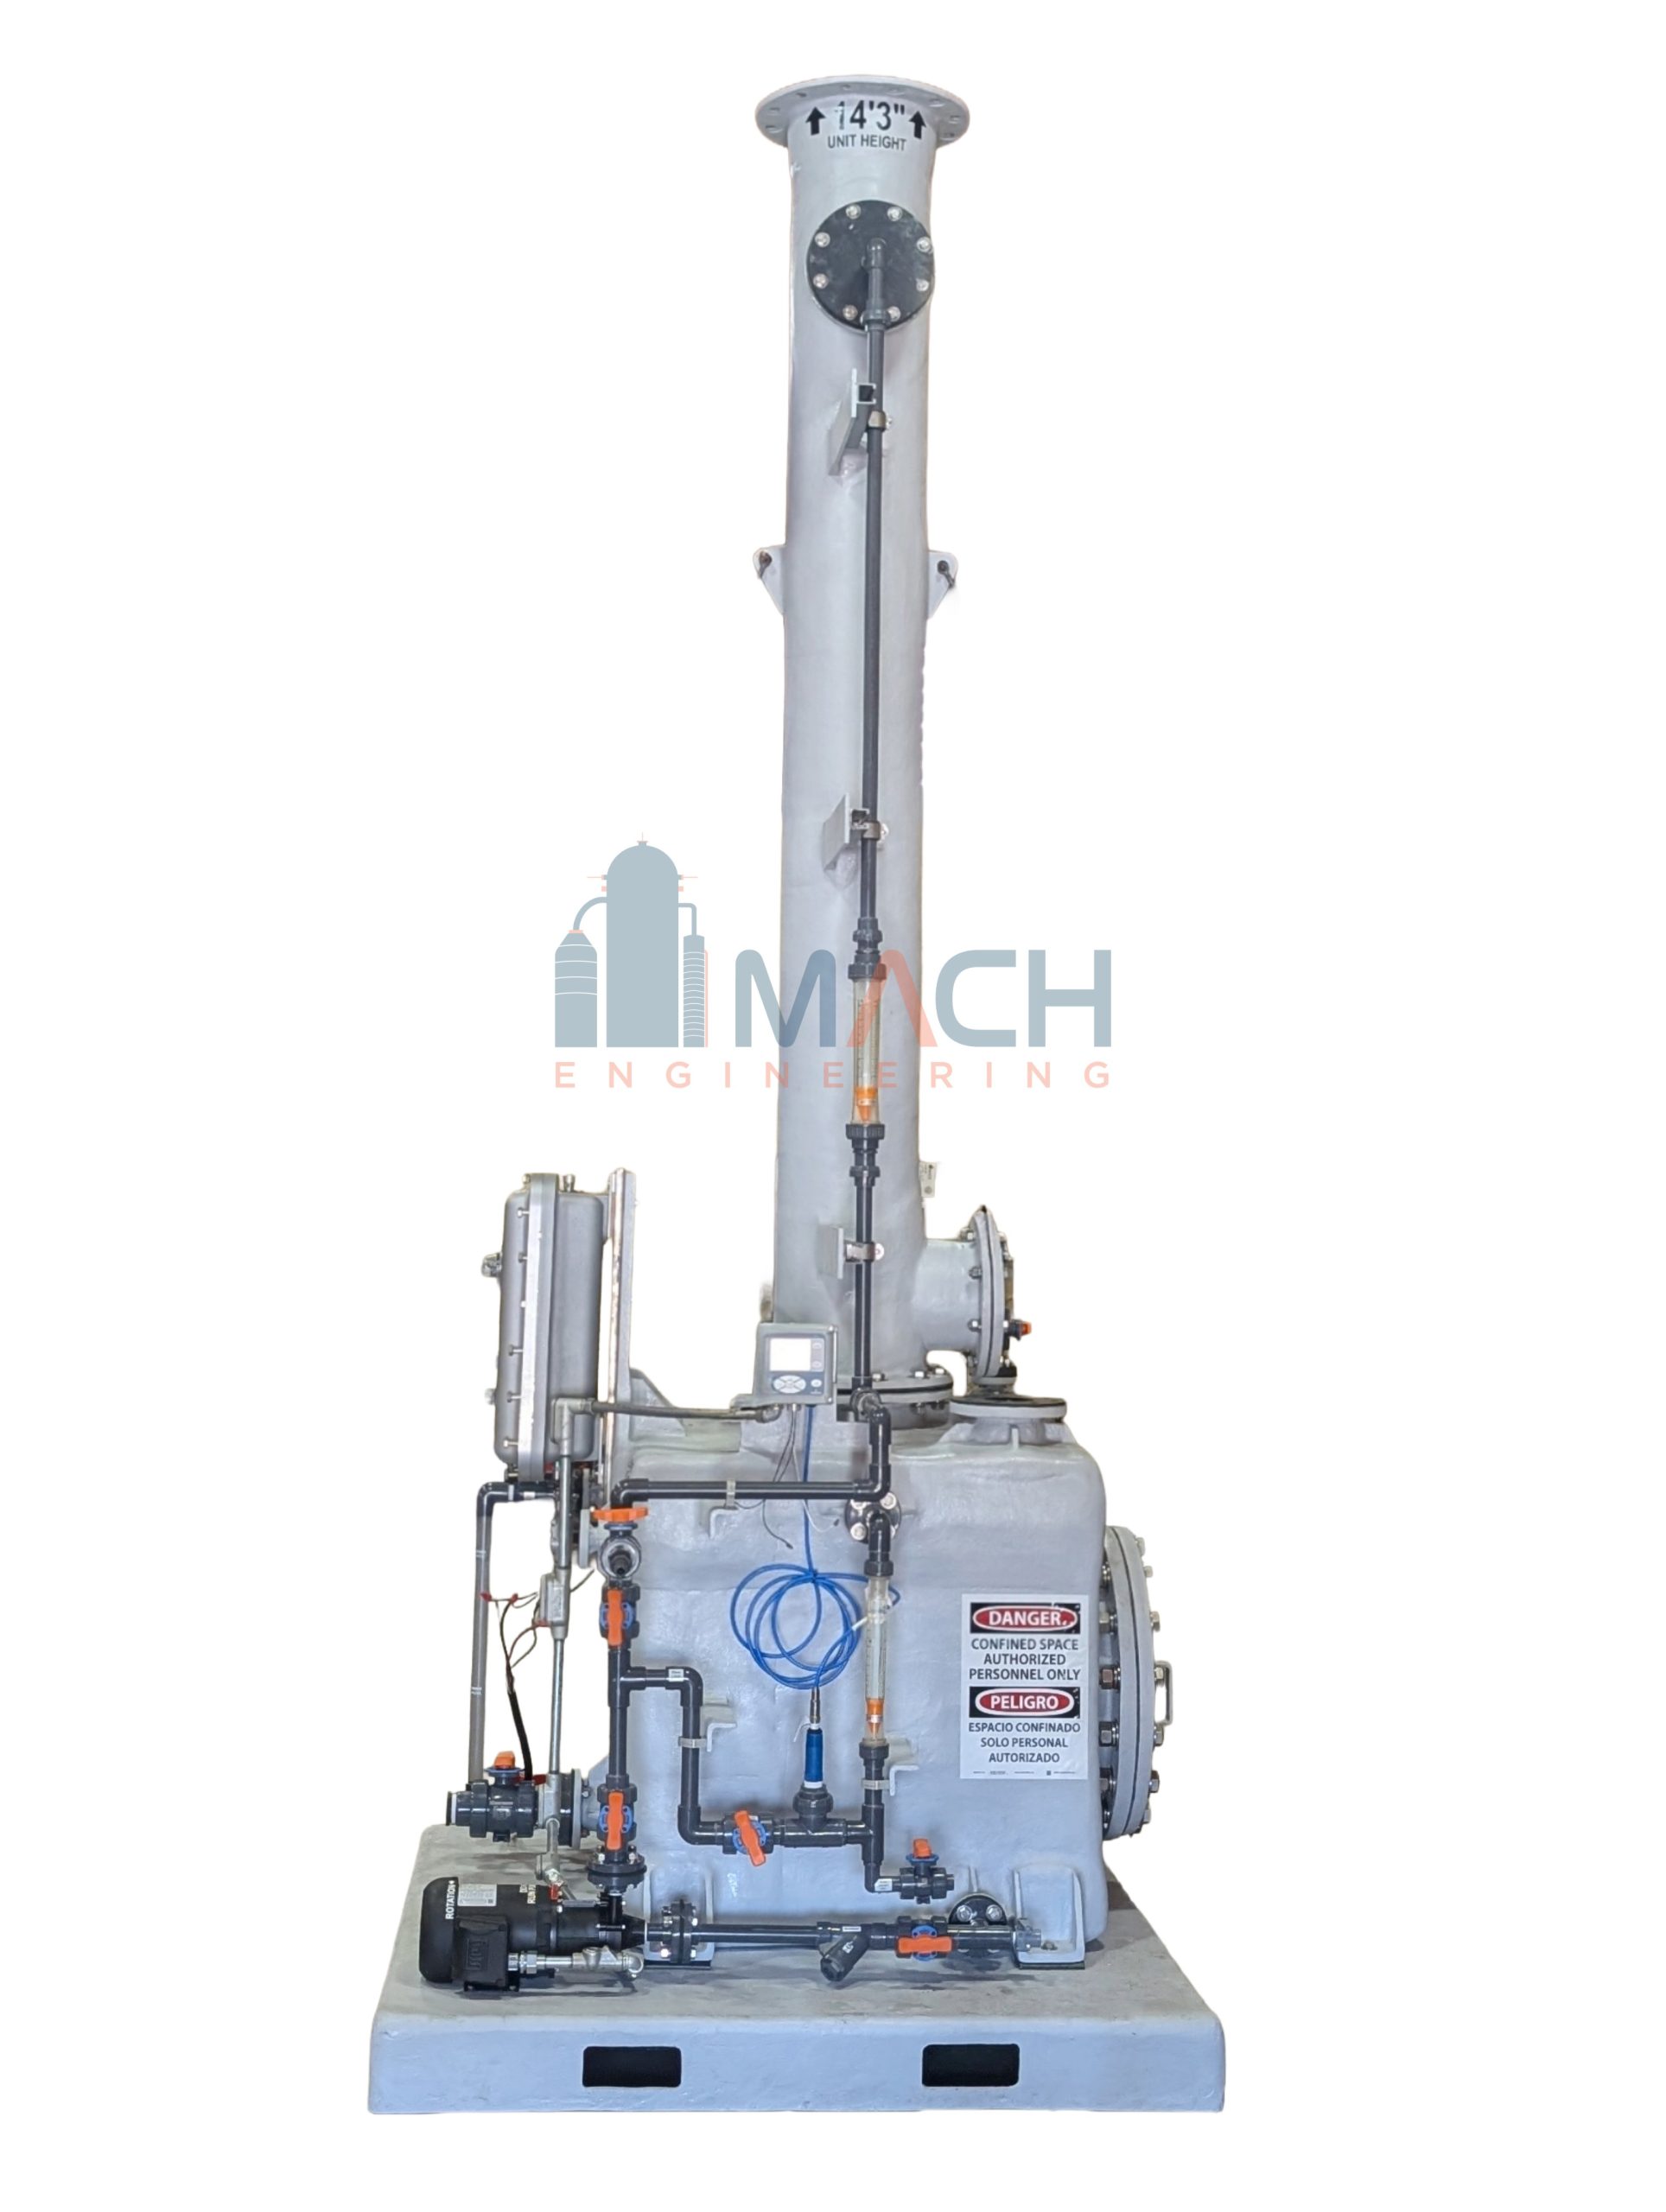
| Design Features | – Skid-mounted system (tower, pump, blower, sump) – pH control system; air dilution valve and rainhat |
Project Location
Deer Park, Texas, USA
Scale of operation
Batch reactor operation (4 times per day, intermittent venting)
Equipment type used (specific scrubber/packing model)
Standalone Caustic Scrubber (FRPS-12), Fiberglass tower with PP packing and internals
Flow rates
164 ACFM reactor vent (design request); ~61 CFM (~438.7 lb/hr) design basis
Removal efficiency rates
99.9% for HNO₃, HCl, NOCl, Cl₂; 40% for NO₂
Installation timeline
12–14 weeks after purchase order
Integration with existing systems
Reactor vent system with nitrogen purge between batches
Special considerations
Batch operation; mercury vapor allowed to pass through; customer handles waste liquid disposal
Pollution reduction percentages
Up to 99.9% removal for acid gases
